


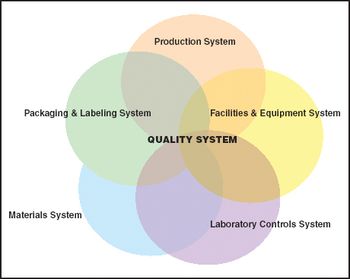
Companies faced with real or threatened FDA sanctions are usually least prepared to react effectively.
A tidal wave of questions floats the need for more upstream automation.
The milestone approval of a gene-edited therapeutic paves the way for gene-editing technologies.
Both adherent and suspension cell culture approaches have their pros and cons, which must be considered for process development.
Companies faced with real or threatened FDA sanctions are usually least prepared to react effectively.
Steam traps are part of a steam-in-place system. The current design allots 18 in. of vertical leg for condensate backup. A design with a sensitive bellows has been proven in laboratory tests to need only 6 in. of vertical leg during the 15 min. of 121?C sterilization. Loads of 1 to 27 lb/h are covered by the capability of the new trap, equivalent to required steam for vessels 20 to 40,000 L.
Nothing beats a good dictionary. It can clarify doubts, settle an argument, or prompt exploration into new areas of learning.
Understand your company's requirements, define responsibilities,and manage your team effectively.
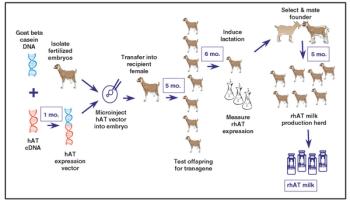
Capital investments in production plants represent a significant portion of the cost of new recombinant drugs
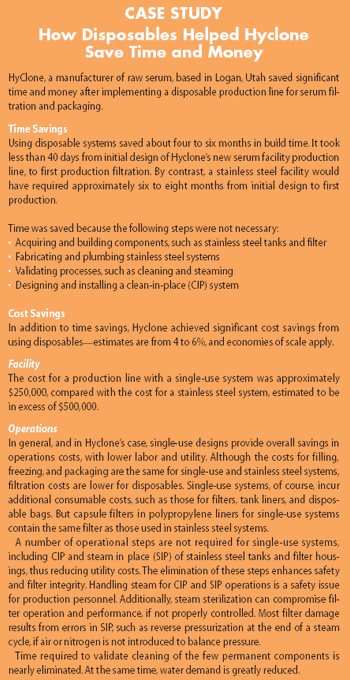
Disposables require less space than conventional equipment, and they can be assembled offsite into complete process trains.
The approvals of two groundbreaking vaccines in the last month is encouraging news. Vaccines have long been undervalued because they haven't been as profitable as other pharmaceuticals. So it's good to see them getting deserved attention that goes beyond fears of flu outbreaks.
"Clinical data is the gold standard" for setting manufacturing specifications, said Patrick Swann, PhD, acting deputy director of the Division of Monoclonal Antibodies at FDA, at a session on specification setting at the AAPS National Biotechnology Conference that was held June 19-21 in Boston.
Several recent approvals highlight progress in developing both prophylactic and therapeutic vaccines.
Using packed columns in process development activities limits the scope for appraising a large and diverse range of media.
The belief that glycosylation is critical to ensuring the functionality of protein therapeutics-and preventing immunogenicity-drives many manufacturing decisions. But is it time to question this industry tenet?
Transgenics can substantially reduce capital investment and lower production costs through economies of scale and more flexible scale-up.
Disposables can be used for media preparation, clarification, filling in downstream processes . . .
Certain areas of the vaccine market appear to be in vogue again, revitalized by blockbusters such as Prevnar, the pneumococcal pneumonia vaccine that reaped $1.5 billion in sales last year, and the human papilloma virus vaccines, which are projected to reach $4 billion per year.
Instead of investing in new facilities, the industry should focus on improving manufacturing technology to increase yields, says Timothy Charlebois, PhD, director of cell and molecular sciences for Wyeth (Madison, NJ, www.wyeth.com). Charlebois made these remarks in his introduction to the session, "Frontiers and Economics of Mammalian Cell Expression," at the BIO 2006 convention."I've seen examples where we took a process that produced 3 grams of protein per liter, and were able to optimize it so that it produced 9.6 g/L," he said, adding that future yields are likely to be above 10 g/L.
One of the major challenges in fungal biotechnology is preventing proteases of the fungi from degrading recombinant proteins.
Alexander Fleming's original process for making penicillin was a low-volume, and presumably, labor-intensive affair. Today, it is a highly optimized, low-budget operation that is carried out only overseas. In other words, says Wei-Shou Hu, PhD, of the University of Minnesota, we engineered ourselves out of a job. Could we do the same with mammalian cell culture? Hu posed this question during a presentation at the BIO conference in April.
The federal government plans to spend $3.3 billion on bird flu initiatives, about half of that on a vaccine.
Anyone who has ever hoisted a glass of a local microbrew has experienced the results of the oldest form of biotechnology?fermentation, the process by which living cells obtain energy through the breakdown of glucose and other molecules. The basic technique of brewing has not changed much in the past 6,000 years, but it is still an excellent illustration of the principles that underlie some of today's most sophisticated biotech production.
To learn more about the processes of fermentation and cell culture used in the production of biopharmaceuticals, you can refer to our advertisers or to the following publications, organizations, and web sites.
Fermentation is an industrial process, but it's probably easier to understand it as something more familiar: raising a living creature. Every fermentation process has to answer several basic questions: Where will the cells live and grow? What will they nourish themselves with? Will the cells live suspended in a mix of water and nutrients (the medium) or do they need to be contained or allowed to attach themselves to a solid base? How will food and air be distributed so all the individual cells get their share? Should all the nutrients the cells need be added at one time, or should the cells be fed additional food as fermentation progresses? How will the progress of fermentation be monitored to ensure the best possible results?
At the heart of modern biotechnology is the ability to manipulate DNA, the astonishing molecule that contains the genetic code of all life on earth. But fermentation and cell culture are also the practical art of keeping cells alive and growing in an artificial environment. As a result, the science of cell culture also includes a healthy focus on the natural processes that keep cells alive.
Many of these terms have more general definitions as well. Those given here are specific to their application in cell culture and fermentation.
As we've shown, biopharmaceutical companies have many options when they choose an expression system: bacteria, yeasts, insect or mammalian cells, and transgenics. Each system has its advantages and disadvantages. Company decision makers must ask themselves several important questions: How much product must be made? How complex is the molecule? Does it require posttranslational modifications to be biologically active? The expression system determines what kind of contaminants will be present and in what quantities. It also determines economic factors: the time scales involved, expression levels obtained, and various regulatory issues. Each potential expression system must be evaluated for its ability to produce economically the maximum amount of biologically active product. Purification methods may be different for products that come from the different host systems. And regulators are more familiar with some systems than with others.
Minimum disruption and maximum gain result when adopting a distributed process control and data management system for a cell culture and fermentation lab.